
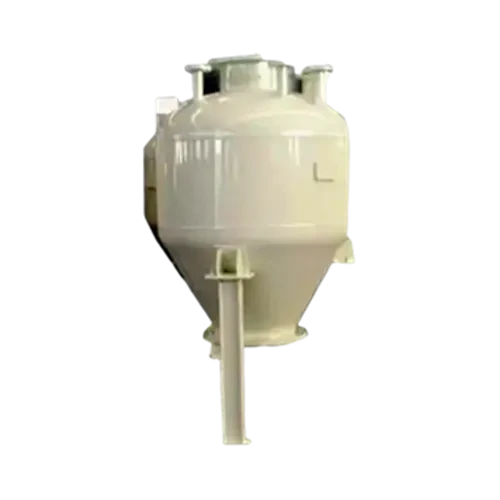
Bin Pump
Features & Advantages of Bin Pump
Sealed Conveying: Conveying takes place inside sealed pipelines, completely eliminating dust dispersion to maintain a clean working environment and meet environmental requirements.
Flexible Layout: Pipelines can be arranged horizontally, vertically or inclined, with almost no restrictions from space and terrain. Powder can be delivered to silos hundreds of meters away or tens of meters high.
Long-distance Conveying: High-pressure air is adopted to efficiently complete automatic and dust-free transfer of powder from collection points to remote silos.
Easy Maintenance: As static equipment, bin pump has no complex moving parts. Maintenance mainly covers valves and fluidizing components, with less maintenance work and fewer fault points than mechanical conveying equipment.
Working Principle of Bin Pump
Filling & Pressure Build-up: The vessel is sealed after full material loading. Low-pressure air is introduced to fluidize powder and build initial pressure.
High-pressure Pushing: The high-pressure air valve is controlled to rapidly boost pressure inside the vessel. Dense-phase material is pushed into the pipeline in slug flow form by strong pressure difference.
Purging Cycle: After discharging, high-pressure air cleans the pipeline. Valves reset automatically and the system enters the next conveying cycle.
 Home
 Products
 About
 Call